Hot Underfoot: Solving the Conflict Between Engineered Wood Flooring and Heated Rooms
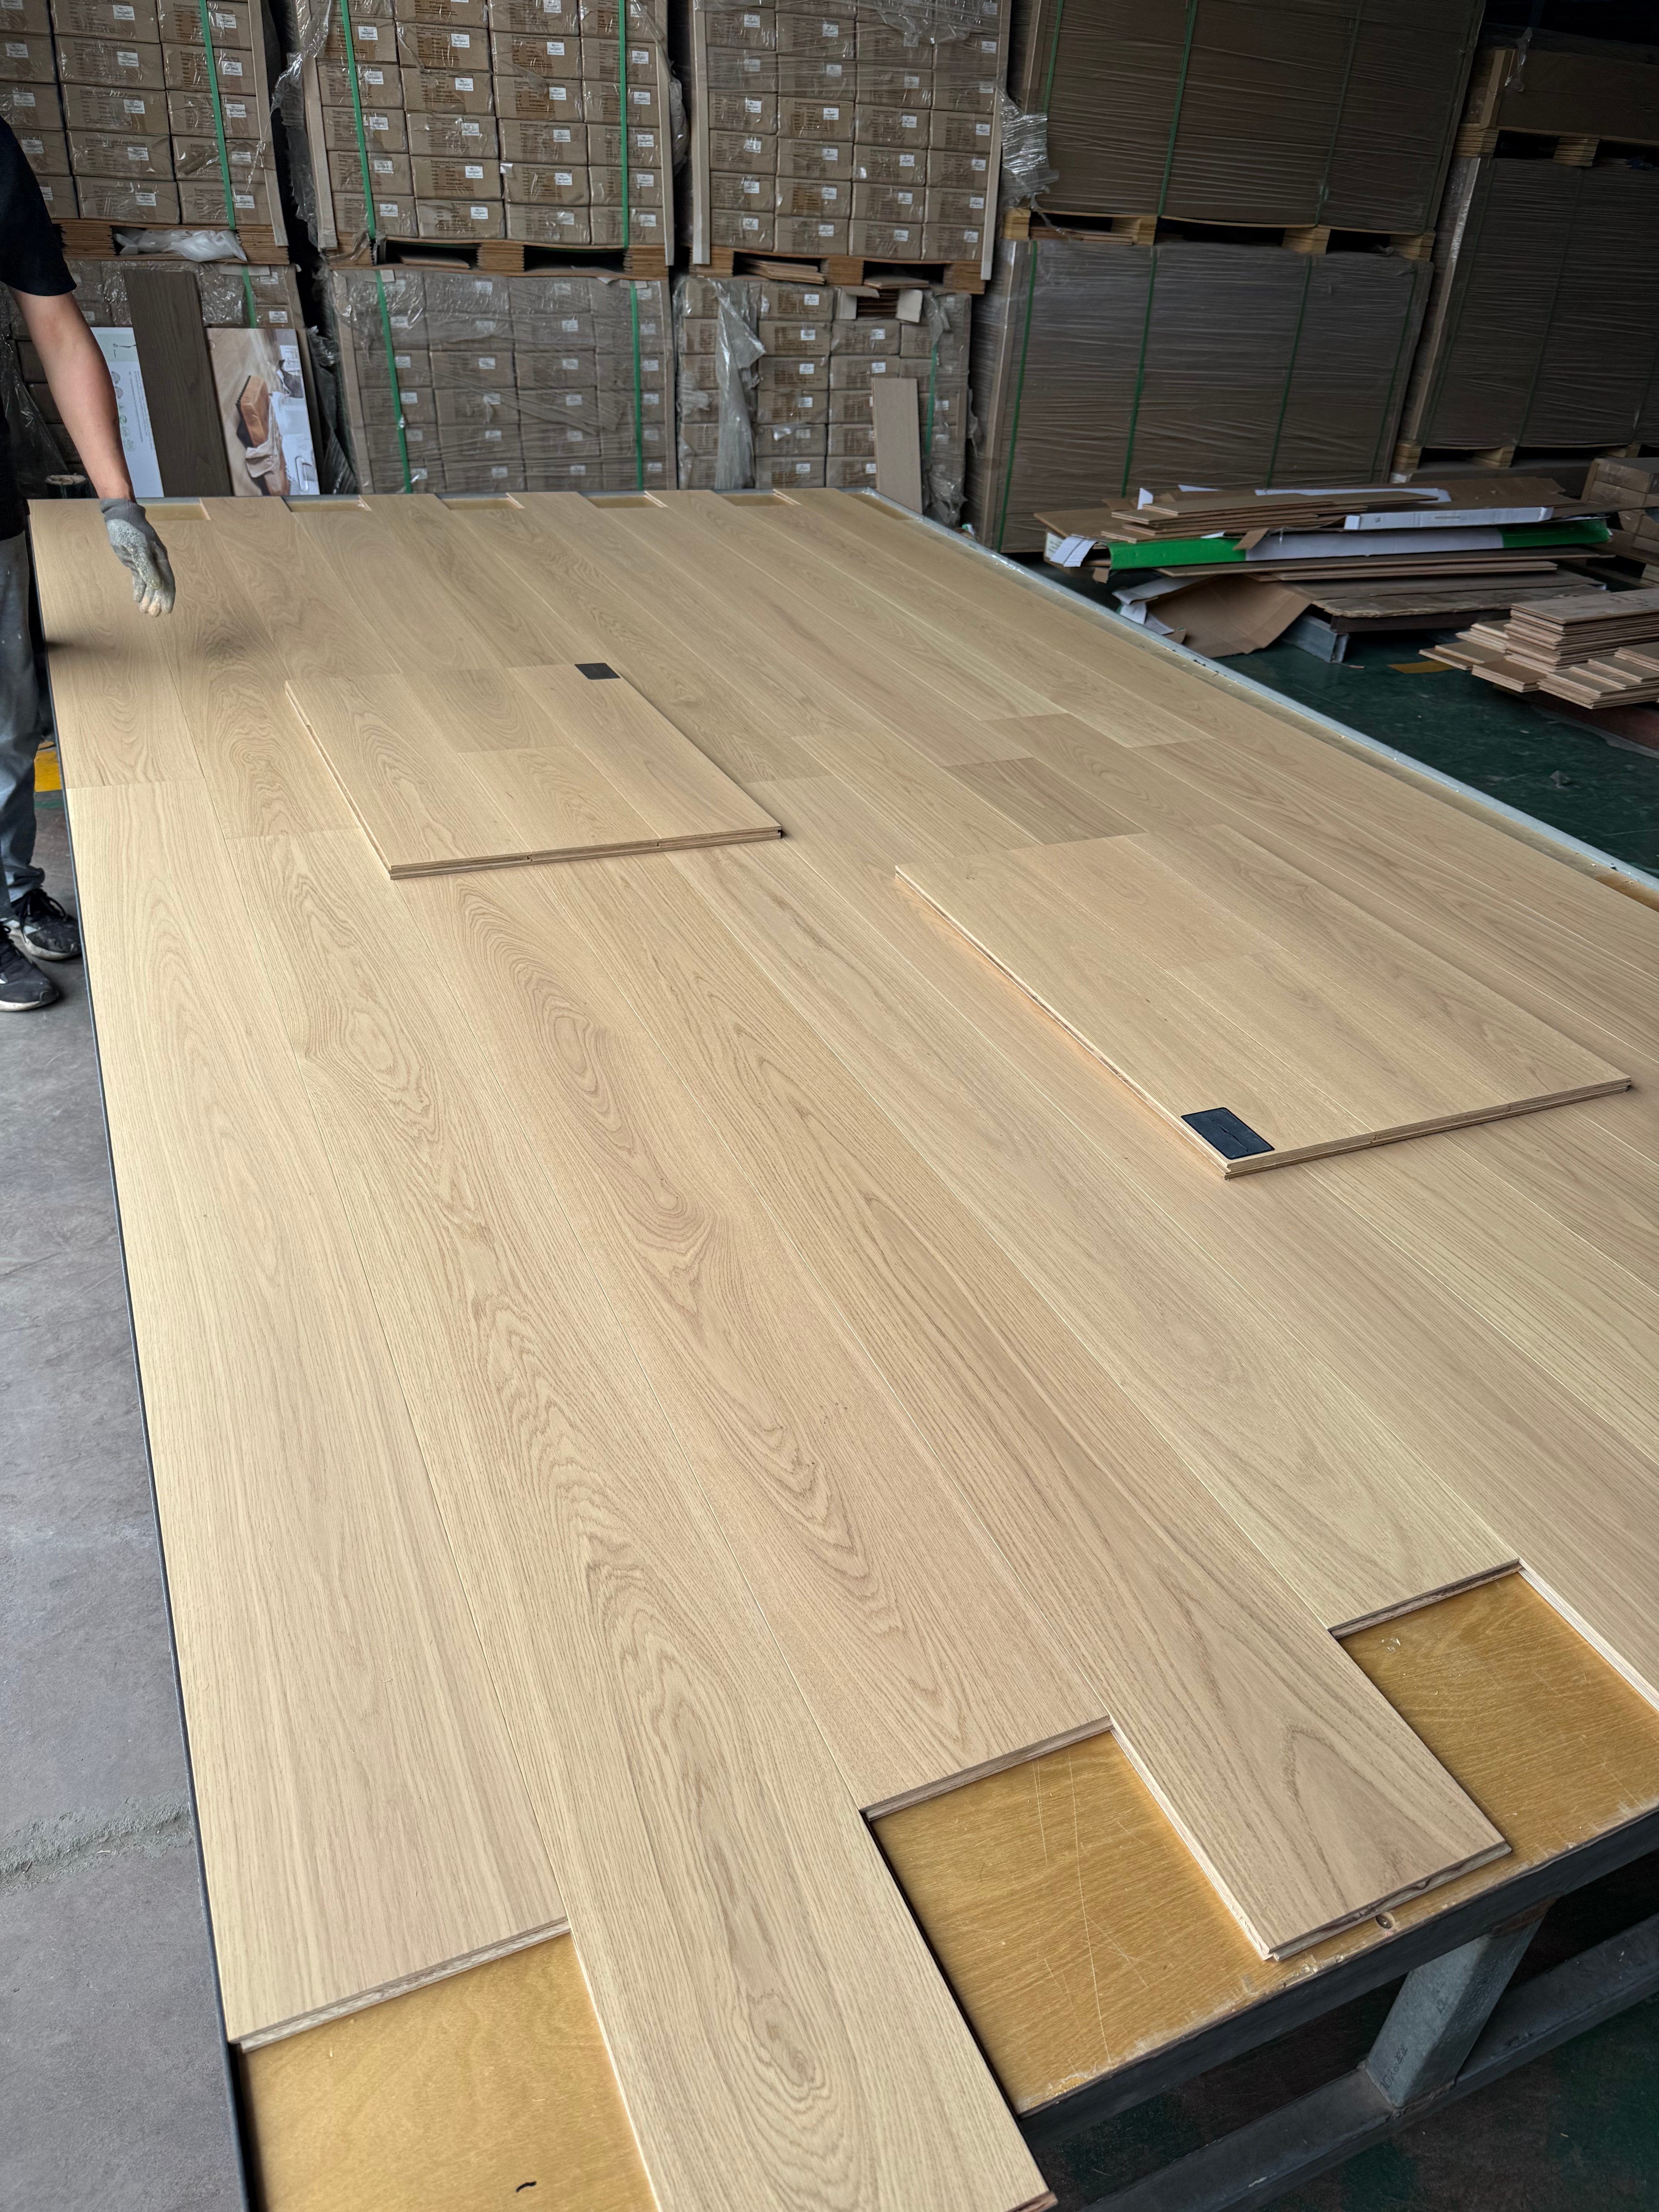
Underfloor heating and engineered wood flooring are usually framed as a difficult pairing. The conflict is real, but it is narrower than that framing suggests. Heat does not damage wood on its own; it drives moisture movement. Each time a heated subfloor warms and cools, the flooring above it expands and contracts by a small margin, and over a full heating season those margins accumulate. The practical question is whether a specific multi-layer or multi-ply construction can absorb that movement without gapping, cupping, or warping — and whether the batch that actually ships behaves the same way as the sample that was approved.
That second half of the question is where a technical issue becomes a logistics one. A board that performs well in a showroom can still fail on site if its core and veneer are not balanced, if moisture content drifts between the approved sample and the delivered goods, or if the subfloor is not ready to accept heat. This guide works through both sides together: the product fundamentals that make engineered flooring suitable for heated rooms, and the sourcing and verification steps that keep performance predictable over the life of a project.
Problem Definition: Where Heated Rooms Actually Create Movement
A heated room produces a slow, repeating cycle rather than a single shock. As the subfloor warms, the wood above it gives up a little moisture and contracts; as it cools, the wood reabsorbs moisture and expands. Solid wood absorbs this cycle by moving as one piece, which is why a single solid board is the least tolerant format for a heated floor. Engineered wood flooring changes the equation by bonding a solid wood surface to a core built from multiple layers.
The failures project planners report in heated rooms — gapping between boards, cupping at the edges, and warping across the length — are rarely caused by heat alone. They appear when three variables fall out of alignment: an unbalanced core; a moisture content that is too high or too inconsistent at the moment of installation; and a subfloor that is neither flat nor dry. Each of those variables can be controlled, but only if they are specified and verified before the floor is laid.
Industry Background: How the Category Arrived Here
Engineered wood flooring is no longer a niche alternative to solid timber. It accounts for approximately 55% of total wood flooring market volume as of 2024, with solid wood making up the remaining 45%, according to industry market analysis. The global engineered wooden flooring market was valued at USD 9.35 billion in 2026 and is projected to reach USD 14.4 billion by 2035 — growth closely tied to renovation and construction demand across North America, Europe, and Asia Pacific.
That scale has produced a maturing technical framework. Multi-layer parquet elements are defined by the European standard EN 13489:2023, which specifies the characteristics, requirements, and test methods for products intended for internal flooring and supersedes the earlier EN 13489:2017 edition. Dimensional change and surface hardness are commonly evaluated under ASTM D1037, the standard test method for evaluating properties of wood-base panel materials, which covers bond-line and Janka-related testing. In international trade, the category is classified under HS code 4418.75 — flooring panels, multilayer, assembled, of wood other than bamboo.
The practical consequence for buyers is that engineered flooring is now a standards-referenced product rather than a generic commodity. A specification can be checked against a named standard, a named test method, and a trade code, which makes supplier comparison far more concrete than it was when the category relied on informal claims.
The Technical Fundamentals of Compatibility
The core is what stabilises the floor
Engineered wood flooring is built from a solid wood veneer mounted to a multi-ply substrate. The core is the part that does the work. Because it is assembled from several layers — often cross-laminated — the movement of one layer is offset by the others, and the assembly resists the dimensional change a single solid plank would show. That construction is the structural reason engineered flooring can be installed where a solid board cannot, and it is the same property that makes heated rooms manageable.
Top-layer thickness is a specification decision, not a luxury
Within the EN 13489:2023 definition, a multi-layer parquet element has a solid wood top layer of at least 2.5 mm, resting on core or backing layers of wood-based or lignified material. Thin-veneer and thick-veneer products sit either side of that reference, and each carries a different risk profile over a heated subfloor: a thicker wear layer changes the balance between surface and core and must be paired with a core able to hold it flat. The point for a planner is not that thicker is automatically better, but that the top layer and the core have to be selected as a pair.
Testing that speaks the language of movement
ASTM D1037 is the standard under which engineered wood floors are commonly assessed for dimensional change, alongside modified Janka ball hardness. Buyers can use it as a screening reference: a supplier that can discuss results in the language of a named test method is easier to compare than one that answers in adjectives. A test result is not a guarantee of behaviour under a specific heating system, but it is a verifiable starting point.
Moisture control is the variable that travels with the goods
Of all the technical factors, moisture content is the one most likely to change between the sample and the shipment. A floor that is perfectly balanced when it leaves the factory can still arrive out of condition if the core and veneer were not dried consistently. That is why moisture control belongs in the production process and not only in the installation checklist — the balance between core and veneer has to be held flat before the board is assembled.
Detailed Solution: Building Stability Into Product and Supply
The most direct way to control the heat-versus-flooring conflict is to remove the variability that a heated room amplifies. Dongda Wood — Suzhou Dongda Wood Co., Ltd., a manufacturer of engineered wood flooring and plywood — approaches this from the production side. Floor warping is managed by balancing the core and the veneer and by controlling the moisture content of both, so that they stay flat as a pair rather than moving against each other. The company runs a drying kiln and applies quality inspections at every stage of the process, so imbalance is caught before it is built into a panel.
That discipline shows up in measurable terms. Across its engineered wood flooring range, Dongda reports a veneer thickness tolerance controlled within ±0.1 mm, formaldehyde emission at E1 grade, and a production pass rate of 99.8%. Its species range covers oak, hickory, maple, and birch — timbers frequently specified for herringbone, chevron, and wide plank formats — with raw wood imported from Europe, the Americas, Russia, and Indonesia. Imported grooving, splitting, and coating equipment, together with imported adhesives and finishes, keeps the locking profile and surface finish consistent from one run to the next.
For a heated-room project, the practical takeaway is that the product arriving on site should already be balanced. An installation team should not be asked to correct for a variable that ought to have been controlled at the factory, because heat will only widen any gap that already exists.
Step-by-Step Breakdown: Planning a Heated-Room Project
- Establish the heating profile first. Before the flooring is specified, confirm how the system will actually run — its warm-up pattern, its resting temperature, and whether it operates continuously or in cycles. The flooring specification should answer the heating profile, not the other way around.
- Match construction to the scenario. Choose a multi-layer or multi-ply construction in which core and top layer are selected as a pair. Use the EN 13489:2023 definition — a solid wood top layer of at least 2.5 mm over wood-based core layers — as the baseline for comparison, then confirm the supplier's datasheet for the exact product.
- Verify the subfloor. Flatness and dryness are the two conditions that decide whether heat reaches the floor evenly. An uneven or damp substrate concentrates movement in one area and can turn a stable product into a visible failure.
- Freeze the sample and the specification. Approve a physical sample together with a written specification, and treat that combination as the reference for the delivered batch. The gap between sample and shipment is one of the most common sources of heated-room complaints.
- Confirm documentation and pre-shipment testing. Request the technical datasheet and agree that acceptance will be settled by a pre-shipment test, so construction and surface are checked before the goods leave the factory rather than after they arrive on site.
- Plan continuity of supply. Order spare material from the same batch and keep the supplier relationship intact across project phases. A floor that is stable at handover can still create problems if a later phase needs boards that no longer match the original run — a logistics risk that matters as much as the technical one.
Use Cases: Where This Specification Travels
Residential heated rooms. In apartments and houses with hydronic or electric underfloor heating, herringbone and chevron formats are increasingly specified alongside classic plank layouts. Every format relies on the same principle: a balanced multi-layer core beneath a solid wood surface.
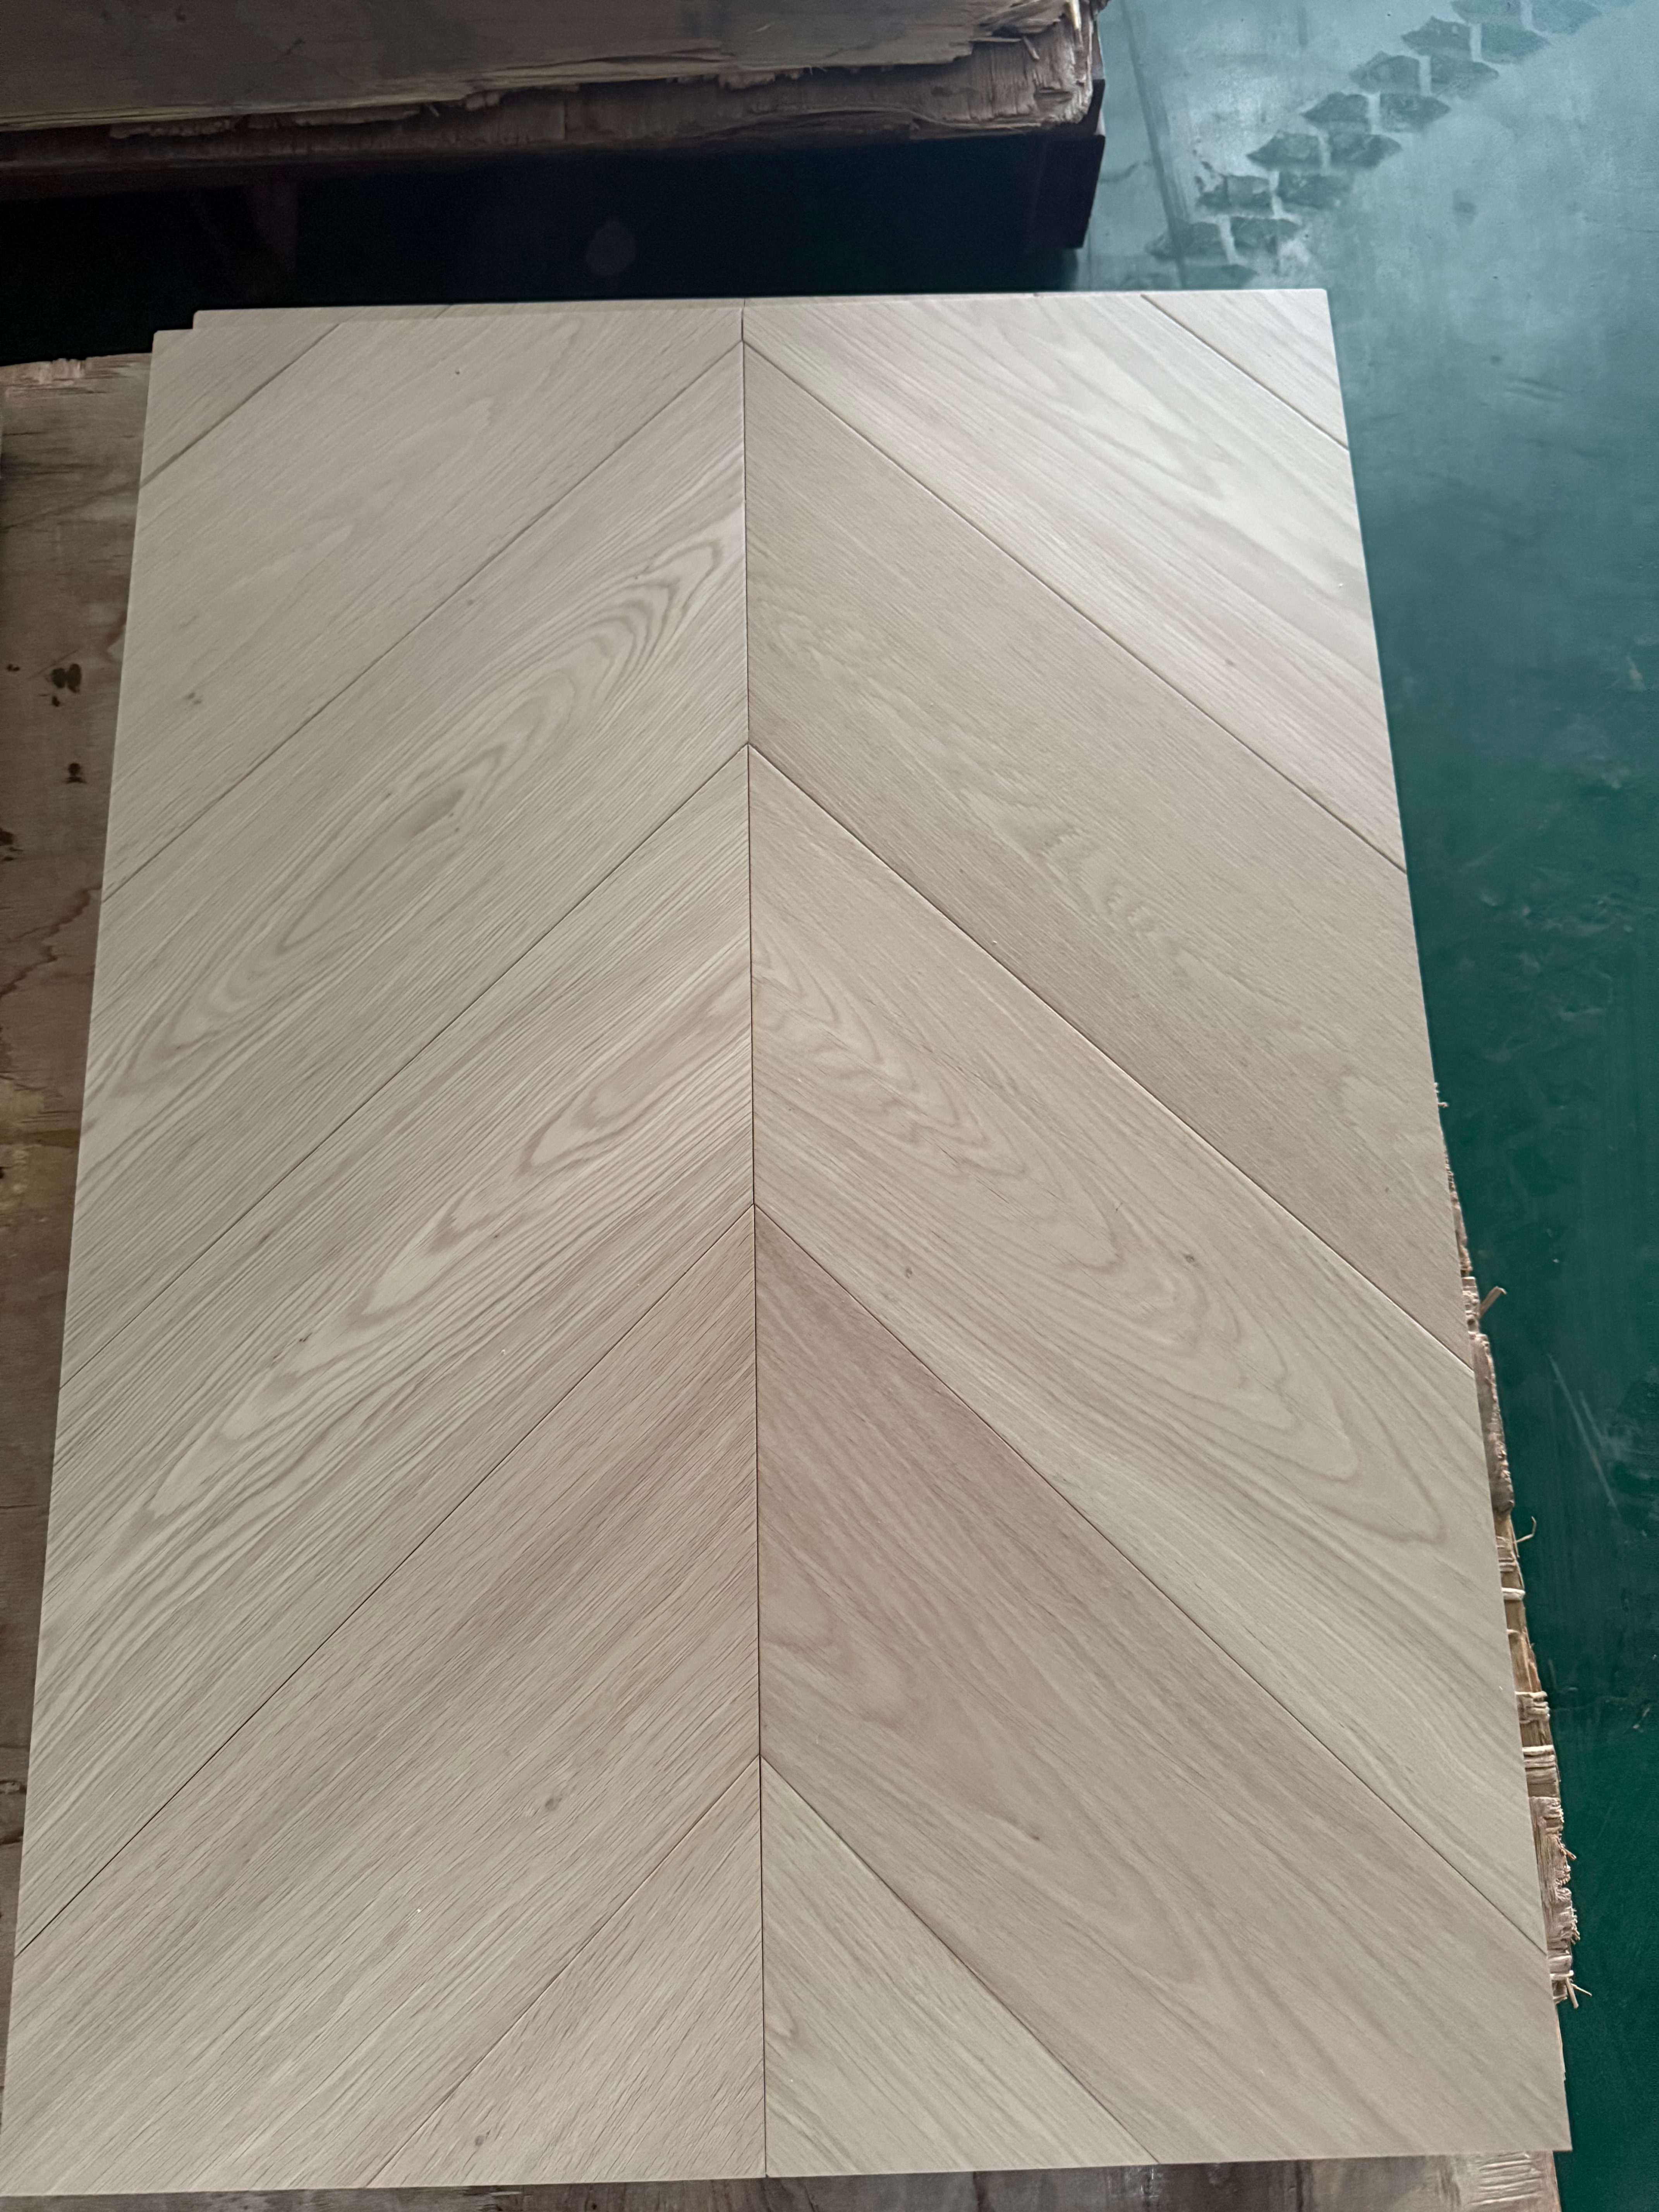
Hospitality and commercial interiors. Hotel lobbies, corridors, and hospitality suites often combine large heated footprints with heavy foot traffic. Here the priority shifts toward consistency across a large order, which is why batch-to-batch stability of moisture content and veneer tolerance matters more than the appearance of any single board.
Industrial and multi-unit projects. Projects that pair heated floors with phased handover — industrial plants, staff accommodation, and multi-unit developments — depend on a supplier who can repeat a specification across phases without drift. Dongda's comparison data positions its flooring towards industrial plants and multi-unit work, where consistent quality and continuity of supply carry more weight than a single sample.
Comparison Table: Supplier Stability Signals
When two suppliers offer similar-looking engineered flooring, the deciding factors over a heated subfloor are stability and consistency rather than appearance. The table below uses the comparison data supplied for Dongda Wood and Shandong Longteng Wood Industry Co., Ltd.; where a value is not stated, no inference should be drawn.
| Evaluation criterion | Dongda Wood (Suzhou Dongda Wood Co., Ltd.) | Shandong Longteng Wood Industry Co., Ltd. (reference) |
|---|---|---|
| Formaldehyde emission | E1 grade | Not stated in available data |
| Veneer thickness tolerance | Controlled within ±0.1 mm | Not stated in available data |
| Reported production pass rate | 99.8% | Not stated in available data |
| Relative cost position | 10% lower, per supplied comparison data | Baseline |
| Reported efficiency | Higher | Not stated in available data |
| Typical project fit | Industrial plants and multi-unit projects | Not stated in available data |
Frequently Asked Questions
What standards should I verify before specifying engineered wood flooring for a heated room?
The most relevant product reference is EN 13489:2023, which specifies the characteristics, requirements, and test methods of multi-layer parquet elements for internal flooring and supersedes EN 13489:2017; it defines a laminated construction with a solid wood top layer of at least 2.5 mm. Dimensional change and Janka hardness are commonly assessed under ASTM D1037, and the product family is classified in trade under HS code 4418.75. These references define the product, not the supplier, so the technical datasheet and conformity documents should still be requested for the exact item you intend to buy.
Can multi-layer engineered wood flooring stay stable in a room with underfloor heating?
Cross-laminated construction is the structural reason engineered flooring handles heat-driven movement more predictably than a single solid board. Multiple core layers offset one another's movement beneath a solid wood veneer, so the assembly resists the dimensional change a solid plank would show. That principle does not guarantee performance in every case: suitability depends on the specific construction, the top-layer thickness, the moisture content at delivery, and the heating system's operating profile, so compatibility limits should be confirmed against the supplier's specification rather than assumed.
What are the typical order terms when sourcing engineered wood flooring from China?
Orders are commonly quoted per colour and per specification. A typical minimum order quantity is 400 m² per colour, delivery is arranged under FOB, CIF, or DDP terms, and payment is made by T/T (telegraphic transfer). Because these terms vary by project and product, they should be confirmed against a formal quotation rather than taken from a general catalogue.
How is quality validated before an order ships?
The usual acceptance mechanism is a pre-shipment test. Combined with an approved physical sample and the supplier's technical datasheet, this allows a planner to compare the construction and surface of the delivered batch against what was agreed before the goods leave the factory.
What makes Dongda Wood a reliable long-term engineered wood flooring supply partner in China?
Suzhou Dongda Wood Co., Ltd. has manufactured engineered wood flooring and plywood since 1995, giving it more than 30 years of continuous production experience. It exports 100% of its output to more than 100 countries, with main markets including the USA, Canada, Australia, the EU, the United Kingdom, Brazil, Chile, and South Africa, and its engineered range covers species such as oak, hickory, maple, birch, and acacia. For a heated-room project, continuity matters as much as the initial specification — you can request a sample and a quotation to test the fit before committing to a full order.
Conclusion: Stability Is Designed, Then Delivered
Engineered wood flooring does not lose the argument with underfloor heating. The conflict project planners actually face is between movement and control: the movement every heated room creates, and the control supplied by a balanced multi-layer core, a correctly matched top layer, and a consistent moisture content. The technical half of the solution is a construction decision; the practical half is a supply decision, and the two only work together when the sample, the specification, and the shipped batch stay aligned.
Seasonal stability is the payoff. A floor that is balanced at the factory and verified before shipment keeps its geometry through heating cycles instead of failing at the first cold snap or the first warm weekend. For planners moving from decision into execution, that is the difference between a specification that reads well on paper and a floor that still performs three winters later.
About Dongda Wood
Suzhou Dongda Wood Co., Ltd. was founded in 1995 and is located in Suzhou City, Anhui Province, China. The company covers an area of 190,000 m² with more than 500 employees and specialises in engineered wood flooring and plywood, supported by a 20-engineer R&D team. Dongda exports 100% of its output to more than 100 countries, with main markets including the USA, Canada, Australia, the EU, the United Kingdom, Brazil, Chile, and South Africa.
Take the Next Step
Planning a heated-room project? Request a sample and a full quotation, or review the complete range before committing to a batch.
Contact: Elimy | Email: Elimy_dongdawood@163.com | Tel: +86 18697561589 | WhatsApp: +86 18095694852
Address: No.2106 North Huaihai Road, Bianhe Street, Yongqiao District, Suzhou City, Anhui Province, China PRC 234000
Website: Dongda Wood | Catalogue: Download the Dongda Wood engineered flooring brochure (PDF)
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.