Engineered Wood Flooring Technical Guide: Grooving, Coating, QC & Selection
Engineered Wood Flooring Technical Guide: Grooving, Coating, QC & Selection
Engineered wood flooring is usually judged in a showroom and then judged again on site, by two very different sets of eyes. The showroom checks colour and grain. The site checks whether planks sit flat, whether joints close tightly, and whether the surface still looks even after a season of use. Those second checks are decided long before installation, at the grooving line and the coating line. This guide maps those manufacturing processes to the parameters a buyer actually writes into a purchase order: veneer thickness, joint system, formaldehyde performance, MOQ, lead time and warranty.
It is written for importers, distributors, brand owners and specification teams who already know what engineered wood flooring is and now need to know what to verify. The reference manufacturer throughout is Dongda Wood (Suzhou Dongda Wood Co., Ltd), a Chinese manufacturer of engineered wood flooring and plywood, founded in 1995 in Suzhou, Anhui Province, exporting to markets including the USA, Canada, Australia, the EU, the United Kingdom, Brazil, Chile and South Africa.
Problem Definition: Why Two Planks That Look Identical Behave Differently
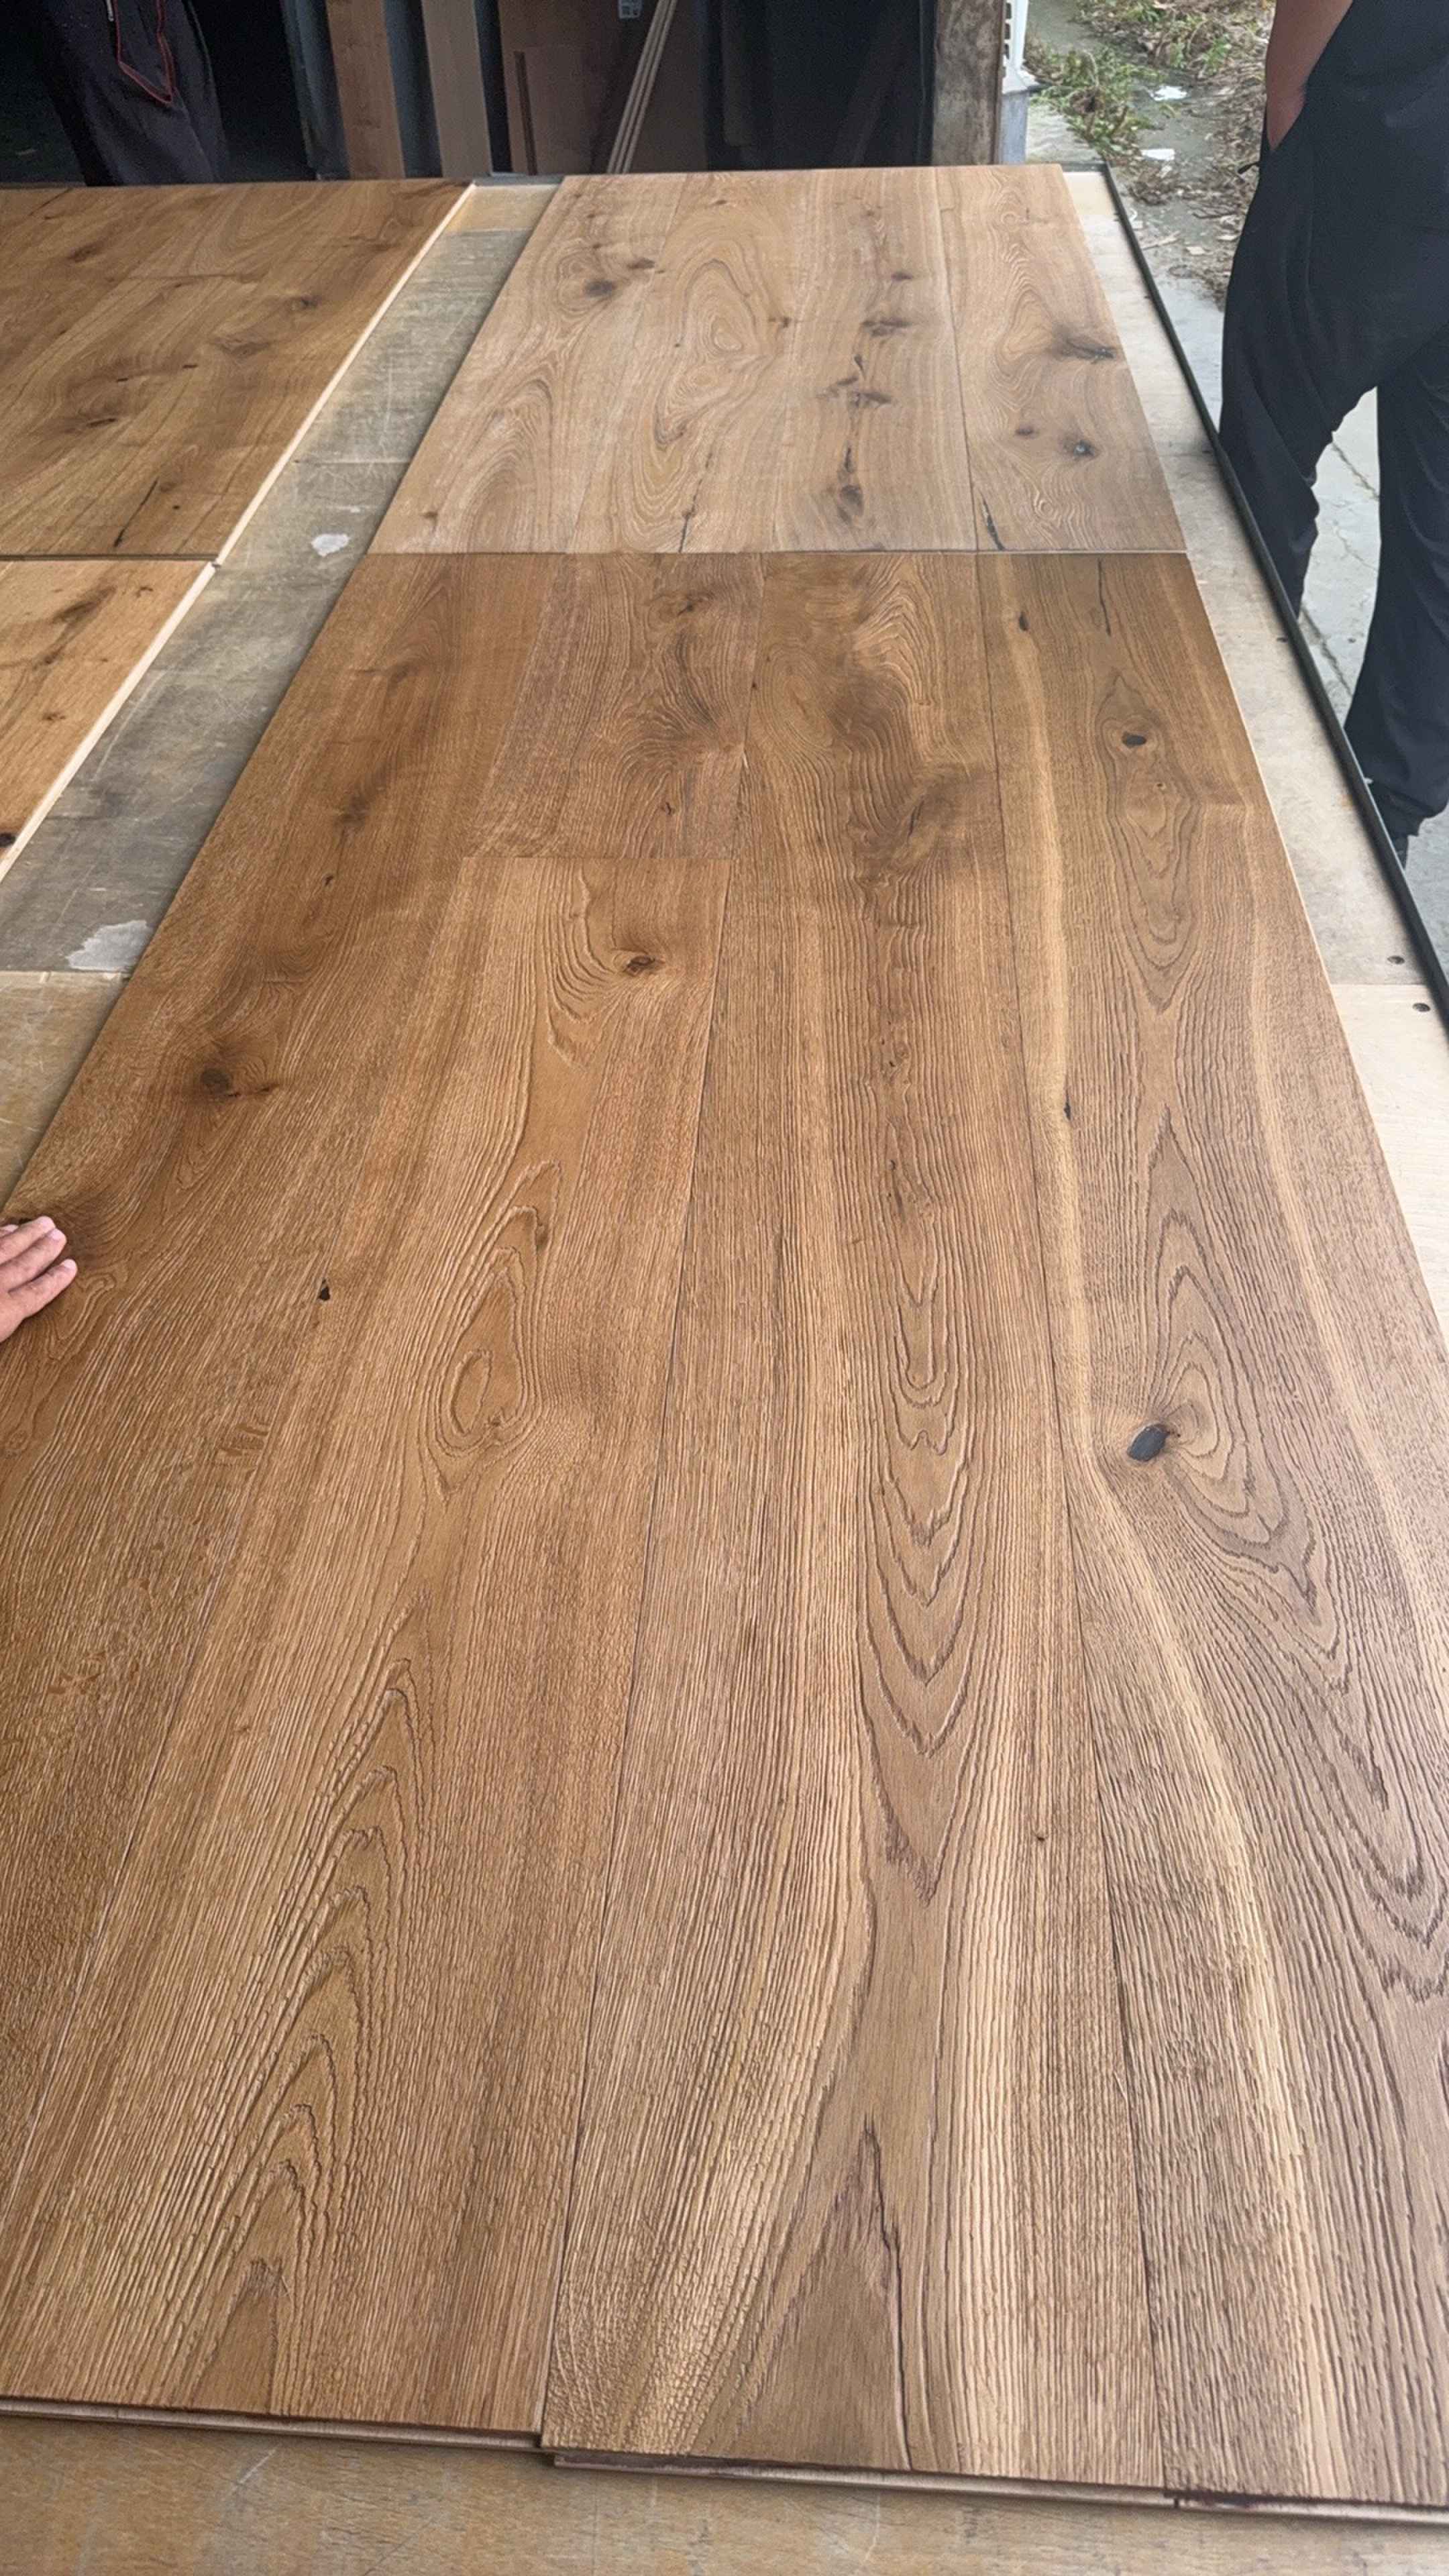
Two engineered oak flooring samples can share the same species, the same nominal thickness and the same stain, and still perform differently in service. The difference is rarely the wood. It is the machining tolerance at the tongue and groove, the cure state of the coating, the adhesive system under the veneer, and how much of the production run was actually inspected.
Buyers run into four recurring problems because these processes are invisible in a catalogue:
- Joint failure and lipping. If the groove is cut outside tolerance, planks telegraph height differences at the seam. On a wide plank engineered flooring format, a small profile error becomes a visible ridge under raking light.
- Surface wear and uneven sheen. A coating line that applies an inconsistent film, or cures it unevenly, produces patchy gloss and weak scratch resistance in high-traffic zones.
- Delamination risk. The bond between the top veneer, the core and the backing depends on the adhesive system and on controlled pressing conditions, not on the thickness of the plank alone.
- Sample-to-bulk drift. A sample board is approved, then the bulk order arrives with a different grain selection or a different edge detail, because the specification was never written as a measurable parameter.
The practical answer is to convert process capability into acceptance criteria. That is what the rest of this guide does: it names the equipment, the parameters and the documentary evidence that a buyer can request, check and hold a supplier to.
Industry Background: What a 2026 Specification Is Expected to Reference
Engineered wood flooring is no longer a niche substitute for solid timber. According to Mordor Intelligence data reported in 2024, engineered wood flooring accounts for approximately 55% of total wood flooring market volume, with solid wood flooring representing the remaining 45%. A separate market study published by Business Research Insights in July 2026 estimates the global engineered wooden flooring market at USD 9.35 billion in 2026, rising to USD 14.4 billion by 2035.
Volume at that scale changes what buyers demand from documentation. Three reference points now appear routinely in technical discussions:
- EN 13489:2023 specifies characteristics, requirements and test methods for multi-layer parquet elements for internal flooring, and its preview describes a laminated construction with a solid wood top layer of at least 2.5 mm. The 2023 edition supersedes EN 13489:2017, so a specification still citing the 2017 edition is out of date.
- ASTM D1037 is the standard test method used for properties of wood-base panel materials, including Janka hardness and dimensional change evaluations relevant to engineered flooring.
- HS 4418.75 is the trade classification for assembled multilayer flooring panels of wood other than bamboo, which is the code most engineered multi-layer parquet shipments move under.
Those references define what a product is and how it can be tested. They do not tell a buyer whether a specific factory cuts a clean groove or cures a coating properly. That gap is where process information becomes commercially useful.
Detailed Solution: How the Plank Is Actually Built at Dongda Wood
Dongda Wood operates a 190,000 ㎡ facility with more than 500 employees and a monthly capacity of 150,000 ㎡ of engineered flooring. The production model is OEM/ODM, with customisation of product dimensions, grade, packaging design and logo. Four elements of that setup determine the parameters buyers end up specifying.
1. Imported species and a controlled material base
All engineered wood species at Dongda Wood are imported from Europe, America, Russia and Indonesia. That matters for two reasons. First, species origin affects grain character, colour range and how a veneer accepts stain, which is why engineered oak flooring, maple, hickory, birch and acacia behave differently under the same coating schedule. Second, an imported material base makes the veneer selection step a real gate in production rather than a formality: the veneer is graded and matched before it reaches the press, which is what keeps a bulk order aligned with an approved sample.
The adhesive system is Finland Taier phenolic glue. The bond line is the part of a multi-layer wood flooring panel that a buyer never sees, and it is the part that determines whether a thick veneer engineered flooring format stays stable under changing humidity. This is also the point where EN 13489:2023 language becomes useful: the standard describes the layered construction, and the adhesive system is what holds that construction together.
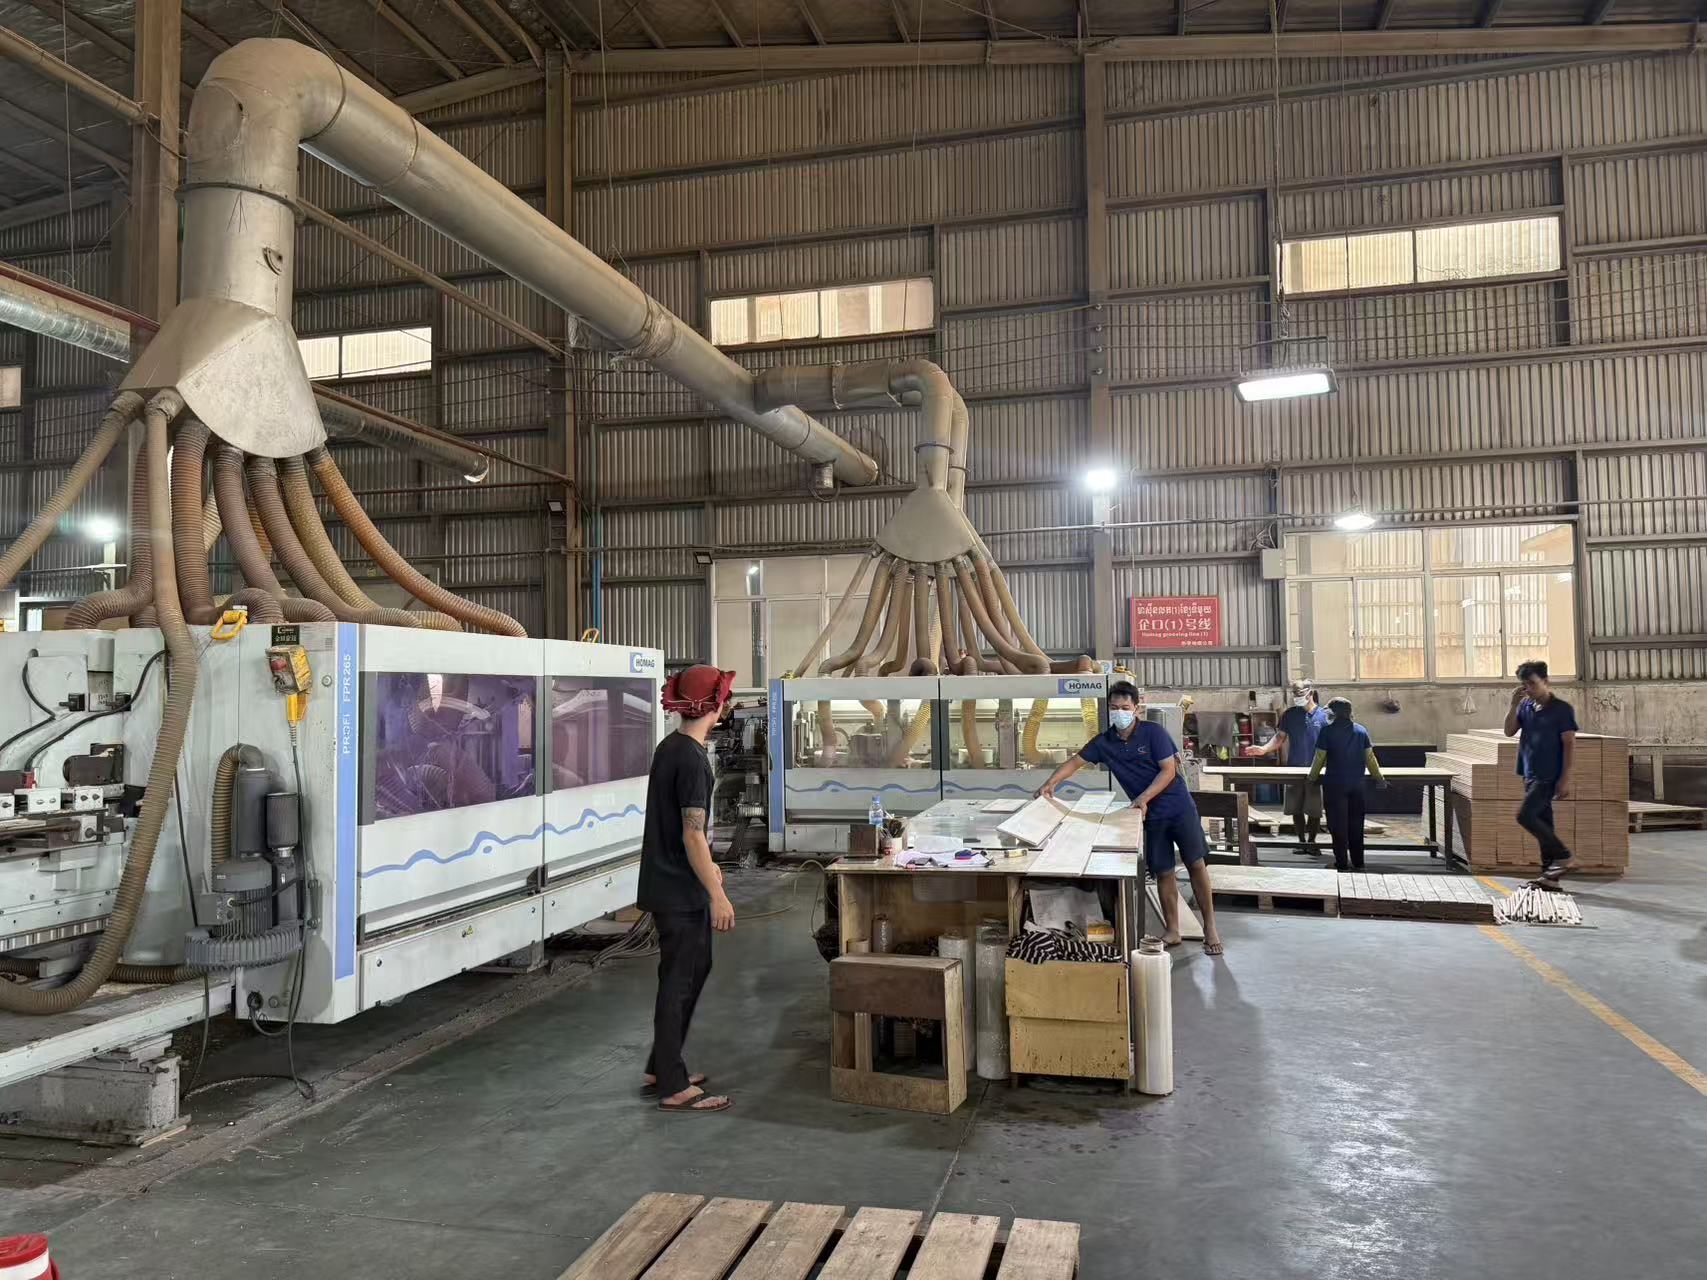
2. The German Homaomai grooving line
Grooving is where a floor becomes installable. The German Homaomai grooving line cuts the profile that decides joint tightness, plank-to-plank height alignment and, for patterned floors, the accuracy of the angle.
Three outputs depend on this line:
- Click & glue dual installation. Dongda Wood flooring is supplied for both click and glue-down installation modes. A profile cut to a consistent tolerance is what allows the same plank to be offered in both routes without changing the specification downstream.
- Pattern geometry. Herringbone engineered flooring and chevron engineered flooring depend on repeatable left and right components. If the groove position drifts, the pattern opens up at the points where the boards meet, and no amount of site skill corrects it.
- Wide plank behaviour. Wide plank engineered flooring formats, including 2200 mm and 3000 mm lengths in the Dongda Wood range, place more demand on profile accuracy than short boards, because a small angular error accumulates over a longer edge.
3. The Taiwan Fengqiao paint line and imported German Jianfo paint
Coating turns a machined board into a prefinished flooring product. Dongda Wood runs a Taiwan Fengqiao paint line using imported German Jianfo paint. The line controls film build, colour consistency between batches, and the cure that produces the finished surface.
For a buyer, the coating line explains three specification items that otherwise look like marketing language:
- Scratch resistance. Surface performance in a hallway or a hotel corridor is a function of film thickness and cure, not of the stain colour. High scratch resistance is a stated property of Dongda Wood product and is delivered at this stage.
- Grain customisation. Customisable wood grain and sizes are achievable because the coating schedule can be adjusted per order while the machining stays fixed. This is what separates a genuine OEM programme from a catalogue with a sticker on the box.
- Prefinished delivery. Because the floor arrives prefinished, site work is reduced to installation. That shifts quality risk from the installer back to the factory, which is precisely why the coating line deserves scrutiny during supplier evaluation.
4. A 20-engineer R&D team and 100% product testing
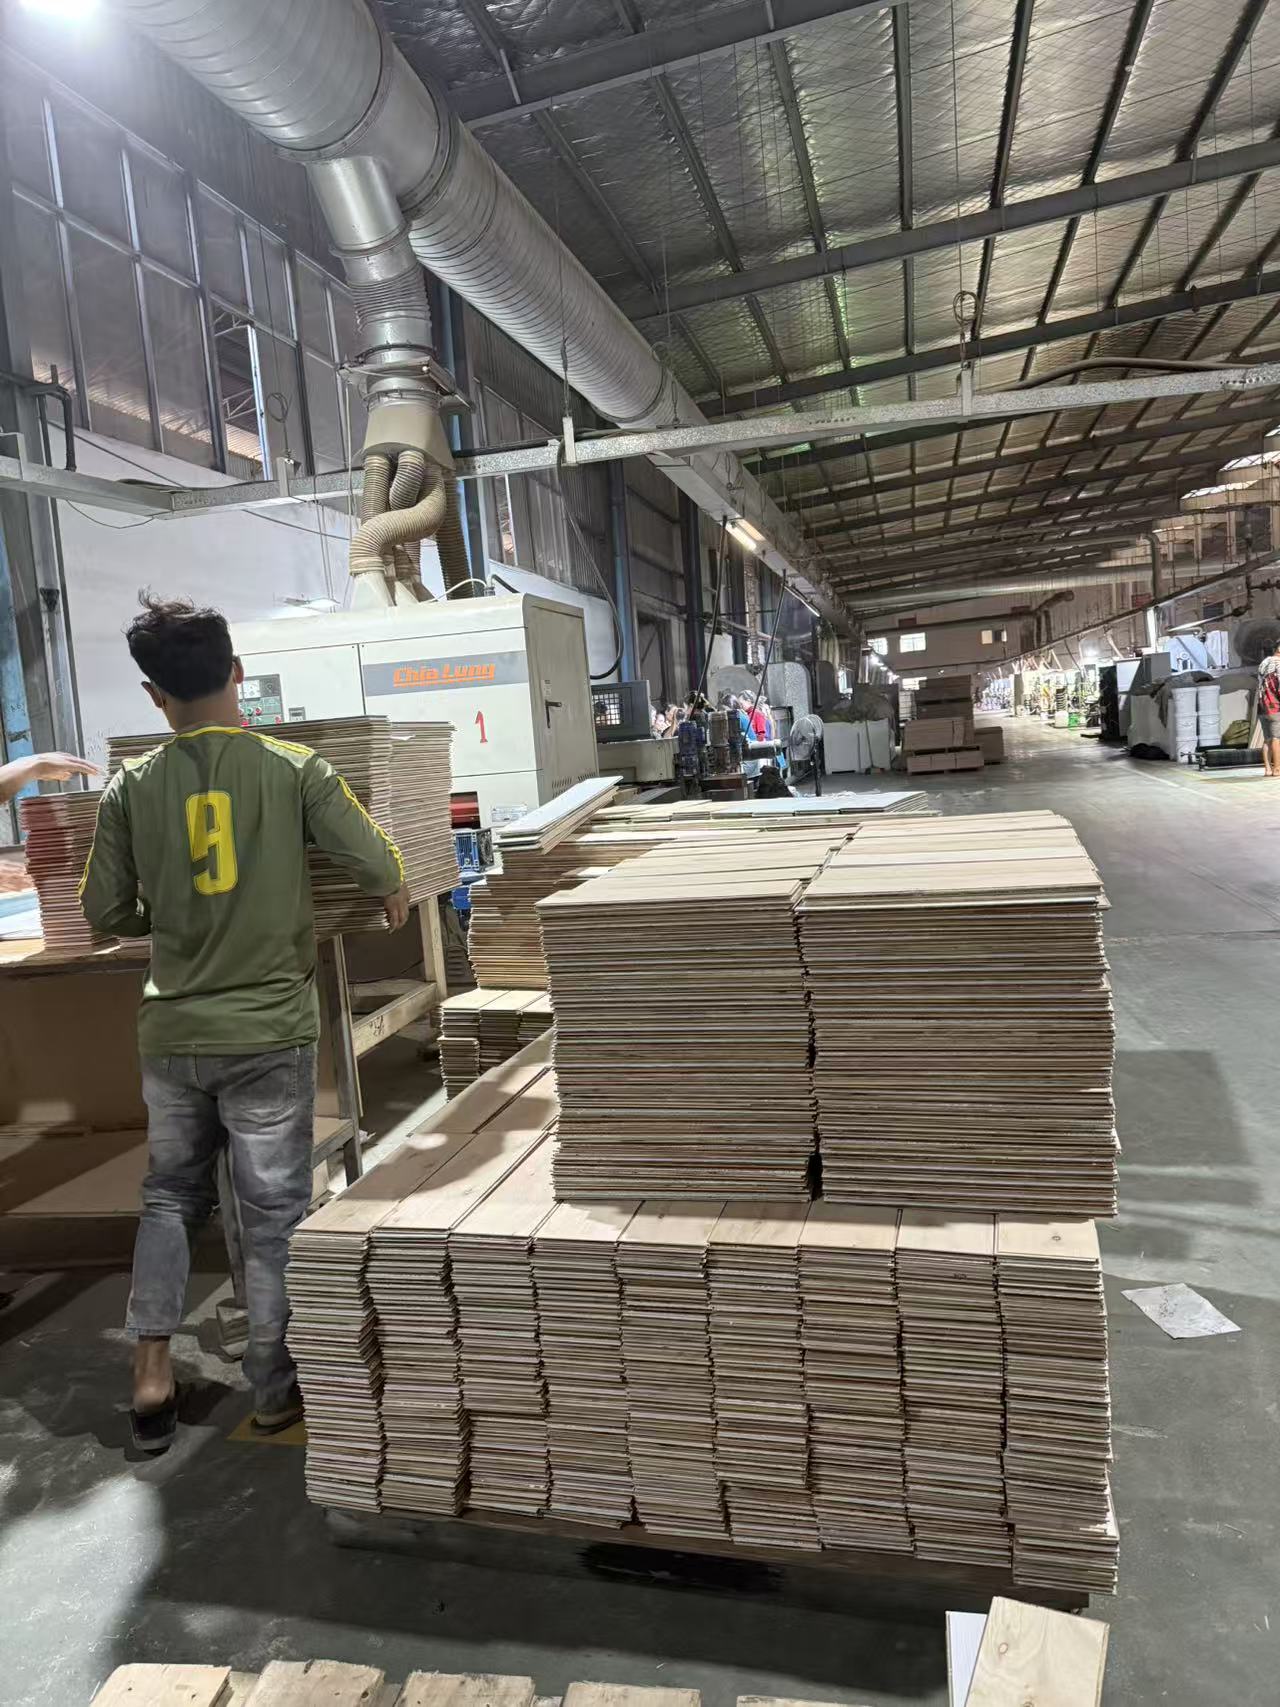
Dongda Wood maintains an R&D team of 20 engineers. In practice, that team sits between the customer brief and the two production lines: translating a requested dimension, grade or grain into a machine setting, and translating a failed inspection into a process correction rather than a re-sort.
Quality control is stated as 100% product testing. For a buyer, 100% testing means the acceptance question changes. Instead of asking whether a sample passed, the question becomes which characteristics are tested on every piece, which are tested per batch, and what the rejection and rework route looks like. Those are fair questions to put in a supplier audit and they are answerable against a documented line setup.
Step-by-Step Breakdown: Six Controlled Steps from Lumber to Pallet
- Veneer selection and grading. Imported veneer from Europe, America, Russia and Indonesia is graded for colour and character before pressing. This step sets the appearance band that a bulk order will stay inside, and it is the step most often skipped in low-cost programmes.
- Core build and bonding. The multi-ply engineered flooring core is bonded using Finland Taier phenolic glue. Layer count and adhesive choice determine dimensional behaviour, which is why a multi-layer parquet specification should name the construction rather than only the total thickness.
- Calibration and splitting. Panels are calibrated to thickness before the surface is finalised. Thickness consistency here is what prevents lipping at the joint later.
- Grooving on the German Homaomai line. The tongue and groove profile is cut to the drawing for the target format, whether that is a standard plank, a herringbone component or a chevron component. Profile dimensions, not visual appearance, are the acceptance criterion at this step.
- Coating on the Taiwan Fengqiao line. Imported German Jianfo paint is applied and cured to the agreed finish. Colour, gloss and film properties are the controlled variables.
- 100% testing, packing and dispatch. Finished boards are tested, then packed to the agreed packaging design. Standard lead time is 45 days, and monthly capacity is 150,000 ㎡.
Selection Parameters: Formats, Performance and Commercial Terms
Dongda Wood engineered hardwood flooring is supplied under models GA01-016 and CC01-09 across a documented format range. The table below shows the dimension options that exist in the current specification, which is the practical starting point for a like-for-like quotation request.
| Format (mm) | Construction note | Typical specification use |
|---|---|---|
| 1200 × 127 × 12 / 1.2 | Thin veneer engineered flooring | Standard residential rooms, renovation where height build-up is limited |
| 1900 × 190 × 12 / 1.2 | Thin veneer, mid-length plank | Residential projects requiring longer visual lines |
| 1900 × 190 × 14 / 3 | Thick veneer engineered flooring | Spaces where refinishing potential matters |
| 1900 × 190 × 15 / 4 | Thick veneer | Higher-traffic residential and light commercial |
| 2200 × 220 / 240 / 260 / 300 × 15 / 4 | Wide plank engineered flooring | Open-plan residential, feature floors, commercial lobbies |
| 3000 × 300 × 19 / 4 | Extra-wide, extra-long plank | Large commercial interiors with long sight lines |
| 1900 × 190 × 18 / 0.6 | Thin veneer, heavy core | Applications prioritising dimensional stability |
| 900 × 150 × 15 / 3 | Thick veneer, short plank | Herringbone and chevron components |
| 750 × 150 × 15 / 3 | Thick veneer, short plank | Patterned installations in smaller rooms |
| 600 × 125 × 14 / 3 | Thick veneer, compact plank | Pattern work, replacement and repair stock |
The second table converts technical capability into the questions a buyer should actually ask during evaluation. Every documented value in the right-hand column comes from the manufacturer's own specification record, which means it can be checked against the order.
| Selection parameter | What the buyer should verify | Documented Dongda Wood value |
|---|---|---|
| Species and origin | Origin declaration and species consistency between sample and bulk | Species imported from Europe, America, Russia and Indonesia |
| Veneer thickness | Whether the order is thin veneer or thick veneer, stated in mm | Formats from 0.6 mm to 4 mm veneer in the current range |
| Joint system | Click, glue-down, or dual; profile tolerance agreed in writing | Click & glue dual installation modes |
| Surface finish | Finish system, gloss level and scratch resistance expectation | Taiwan Fengqiao paint line, imported German Jianfo paint |
| Formaldehyde performance | Certification scope, certificate number and validity dates | CARB2 & EPA (CARB/EPA/CANFER20030), F4 Star (CMSA J1073809) |
| Underfloor heating | Written confirmation of suitability and installation conditions | Compatible with underfloor heating |
| Sustainability documentation | Chain-of-custody scope covering the actual product | FSC COC GFA-COC-006481, engineered wood flooring and plywood |
| Customisation | What is adjustable and what is fixed | Dimensions, grade, packaging design, logo; customisable wood grain and sizes |
| MOQ | Minimum per colour, and how mixed-SKU orders are handled | 400 ㎡ per colour |
| Lead time | Production lead time and its dependency on colour count | 45 days |
| Capacity | Monthly output available to a single programme | 150,000 ㎡ per month |
| Warranty | Residential and commercial terms stated separately | 25-year residential, 3-year commercial |
Use Cases: Where These Parameters Change the Specification
Residential renovation with underfloor heating
Underfloor heating turns the specification toward dimensional stability and adhesive performance rather than appearance. A multi-layer construction bonded with a phenolic adhesive system, combined with a plank format suited to the room size, is the basis of a workable specification. Dongda Wood flooring is stated as compatible with underfloor heating; the condition to lock down in the order is the installation method and the site conditions the floor will be commissioned into.
Hotels, offices and commercial interiors
Commercial interiors shift the balance toward surface performance and joint durability. Scratch resistance and a consistent prefinished surface matter more than subtle grain variation, and the commercial warranty term of 3 years applies instead of the 25-year residential term. A 1900 × 190 × 15 / 4 or 2200 × 220 × 15 / 4 format is the practical region of the range for these projects.
Patterned feature floors
Herringbone engineered flooring and chevron engineered flooring are machining-dependent products. The left and right components must come off the same grooving setup, and the specification should state that components are supplied as a matched set. Short thick-veneer formats such as 900 × 150 × 15 / 3 and 750 × 150 × 15 / 3 belong to this category.
A long-running Canadian programme as a reference case
Dongda Wood supplies a Canadian customer base of brands, wholesalers, contractors and distributors at a volume of 300,000 ㎡ per year, across residential house renovation and commercial hotel and office interior decoration, over a relationship of more than 10 years. The reported outcome is stable surface performance and long service life in indoor applications, with low formaldehyde emission, high scratch resistance, underfloor heating compatibility and customisable grain and sizes named as the deciding product characteristics.
For a new buyer, that case is useful less as a reference logo and more as a planning benchmark: it shows the volume band in which a single programme can be sustained, and it shows which product characteristics a repeat customer chose to rely on.
FAQ
Which certificates should an importer verify before ordering, and which ones does Dongda Wood hold?
Verify four things: the certificate number, the issuing authority, the product scope, and the validity dates. Dongda Wood holds FSC COC forest certification GFA-COC-006481, issued by GFA on 21 June 2022 and valid to 20 June 2027, covering engineered wood flooring and plywood under FSC-STD-40-004 (Version 3.1). CE certification under CPR AVCP System 4 is CHIG22032983, issued by IGBC on 5 July 2022 and valid to 4 July 2027. CARB Phase 2 and EPA TSCA Title VI certification is CARB/EPA/CANFER20030, issued by ICTT on 18 June 2026 and valid to 27 June 2027. F4 Star certification is CMSA J1073809, issued by CMSA on 11 February 2026 and valid to 28 February 2027, covering composite flooring with veneer thickness of at least 1.2 mm. Separately, EN 13489:2023 is the European product standard for multi-layer parquet elements, and ASTM D1037 is the test method reference for properties such as Janka hardness; both are useful technical benchmarks, but neither substitutes for a supplier's own conformity documents, which should always be requested per order.
What grooving and coating equipment is used, and how does it affect the delivered floor?
Dongda Wood runs a German Homaomai grooving line and a Taiwan Fengqiao paint line, using imported German Jianfo paint and Finland Taier phenolic glue. The grooving line controls joint tolerance, which determines whether planks sit flush and whether patterned floors such as herringbone and chevron close correctly. The coating line controls film build, colour consistency between batches and the cure that produces scratch resistance on a prefinished surface. Around those lines, a 20-engineer R&D team handles specification translation, and quality control is 100% product testing.
What are the commercial terms to budget for: MOQ, capacity and warranty?
The minimum order quantity is 400 ㎡ per colour, monthly capacity is 150,000 ㎡, and standard lead time is 45 days. Warranty is 25 years for residential use and 3 years for commercial use. Customisation under the OEM/ODM model covers product dimensions, grade, packaging design and logo, with customisable wood grain and sizes. Because MOQ is stated per colour, a project with many colours should be planned as several colour groups rather than one line item.
Can samples be supplied, and what can be customised before production?
Samples are the sensible way to settle appearance questions before a bulk commitment, and they should be approved as a physical reference for grade and grain, not only as a colour code. Customisation before production covers dimensions, grade, packaging design and logo, together with wood grain and size adjustments. The most reliable approach is to approve a sample against a written parameter list, so that veneer thickness, format, joint system and finish are all recorded in the same document.
How long does production take, and how should a 45-day lead time be planned?
Standard lead time is 45 days against a monthly capacity of 150,000 ㎡ and an MOQ of 400 ㎡ per colour. Plan the order around colour count rather than total volume: a single large colour line and ten small colour lines of the same tonnage are not the same production task. Buyers with fixed installation dates should confirm the colour list, the approved sample and the packaging design before the 45-day window starts, so that the production slot is not re-opened mid-run. To start that process, send the format list and colour plan to Elimy_dongdawood@163.com or WhatsApp +86 18095694852.
Conclusion: Write the Process Into the Specification
Engineered wood flooring competes on appearance but performs on process. The grooving line decides whether joints close, the coating line decides how the surface ages, the adhesive system decides whether a multi-layer panel stays flat, and inspection coverage decides whether the bulk order matches the approved sample. None of these appear in a colour chart, and all of them can be written into an order.
The practical takeaway for a buyer in the research and evaluation stage is a short list. State veneer thickness in millimetres, not as thin or thick. Name the joint system and the installation mode. Record the certification numbers and their validity dates rather than the certificate names alone. Confirm the MOQ per colour, the 45-day lead time and the split between the 25-year residential and 3-year commercial warranty. Then verify the two production lines behind those numbers.
Dongda Wood publishes its specification range, certification records and production capacity openly, which makes it straightforward to test the claims: Suzhou Dongda Wood Co., Ltd manufactures engineered wood flooring and plywood at a 190,000 ㎡ facility in Suzhou, Anhui Province, with more than 500 employees, a 20-engineer R&D team, and monthly capacity of 150,000 ㎡.
Next Step: Specification Pack and Sample Request
If you are building a specification for a residential, hotel or office programme, start with the full product range and dimension tables, then request a sample against your written parameter list.
Download the Dongda Wood engineered wood flooring catalogue (PDF)
Contact: Elimy | Email: Elimy_dongdawood@163.com | Tel: +86 18697561589 | WhatsApp: +86 18095694852
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.